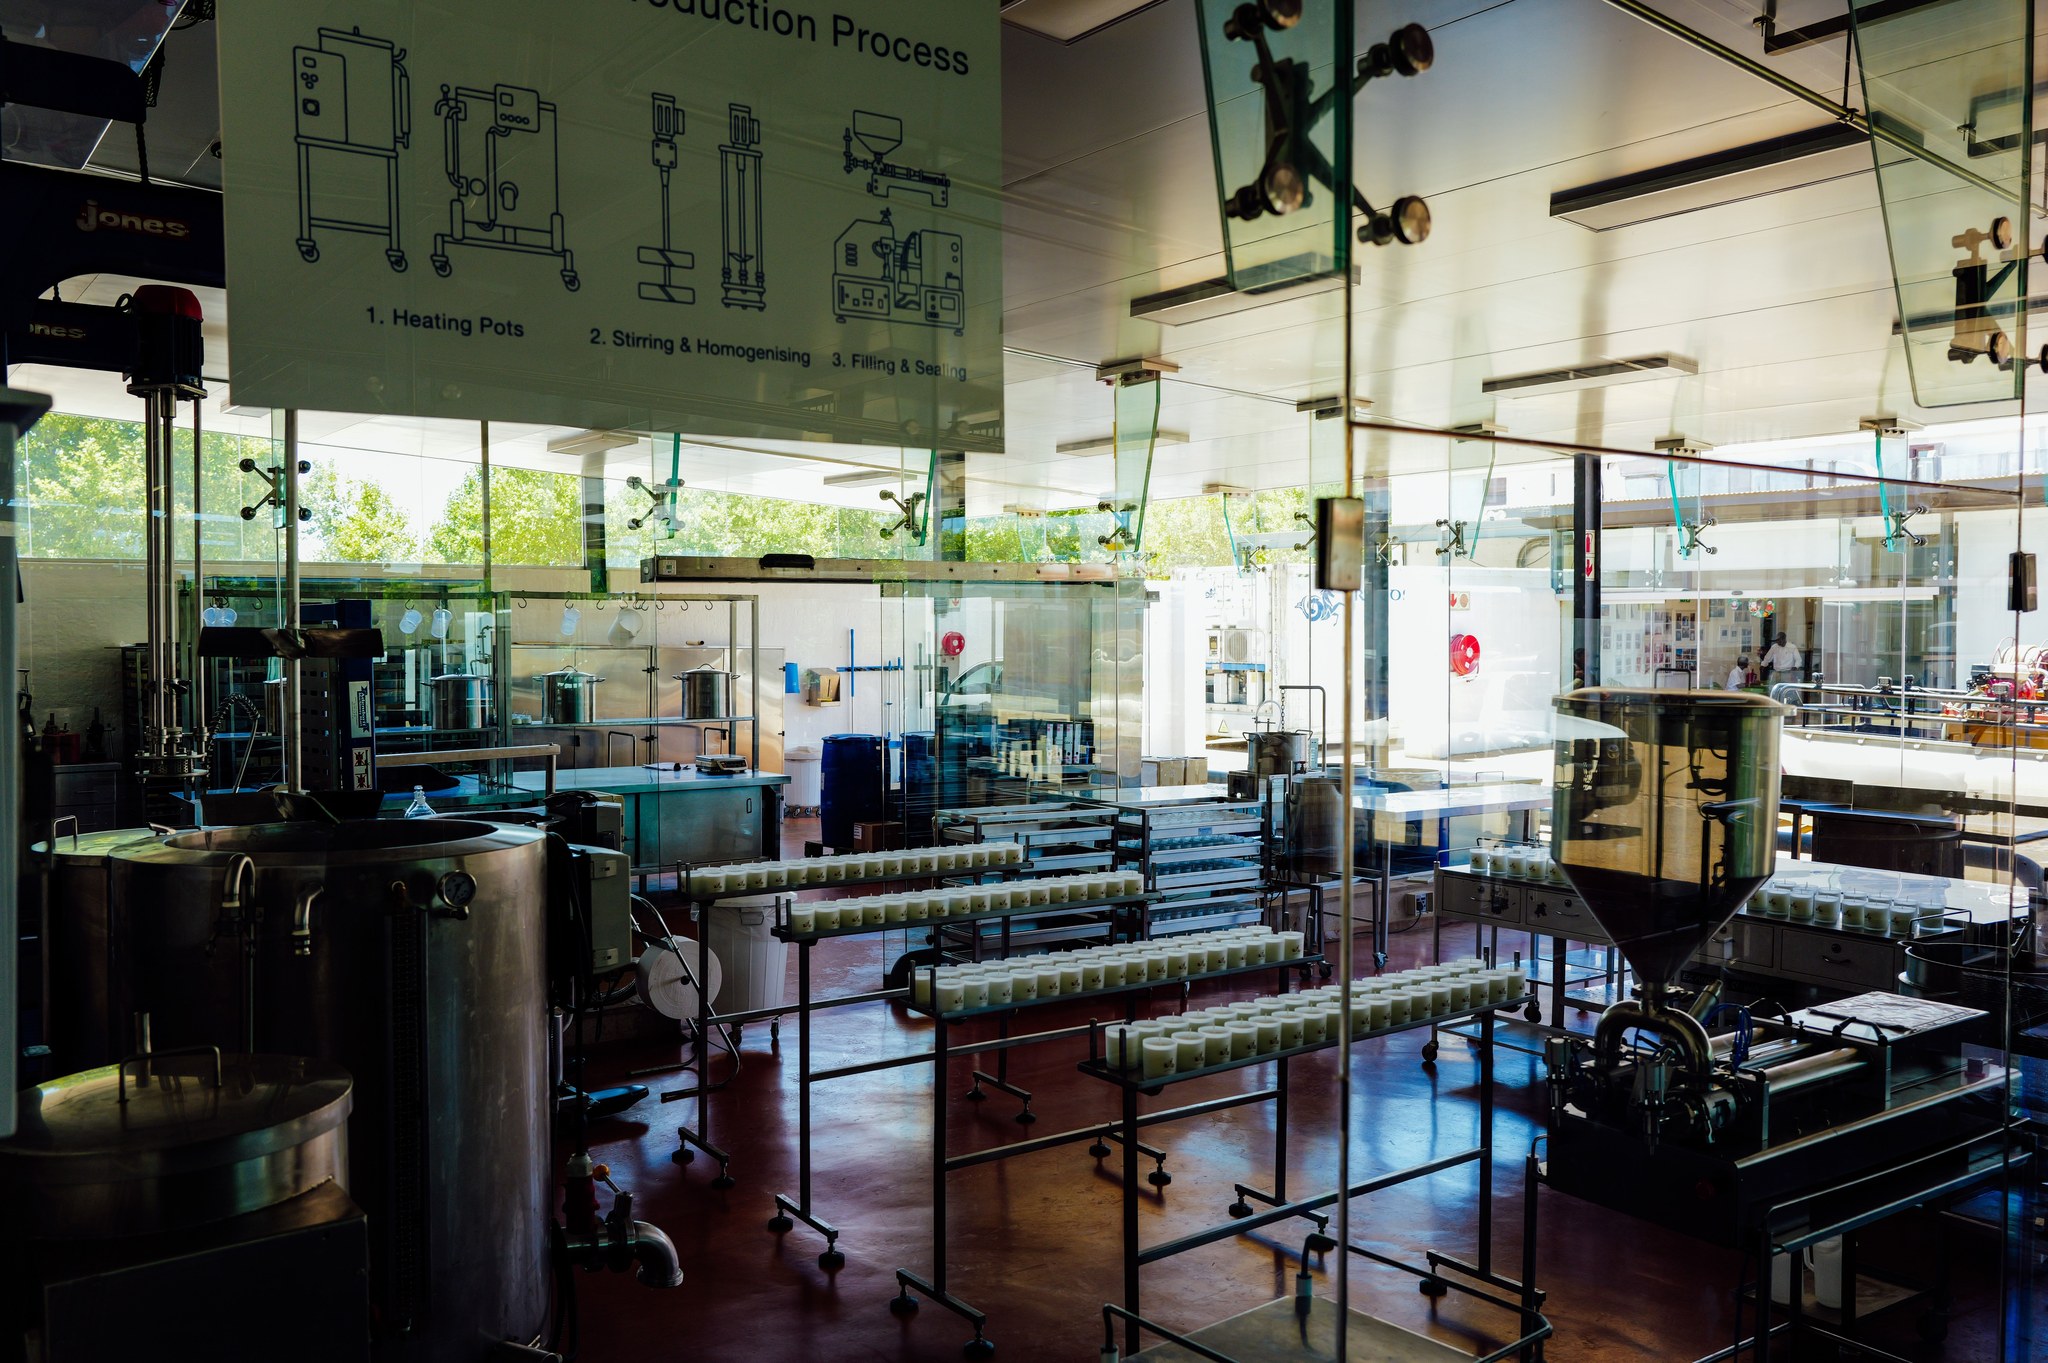
If you’re starting a supplement brand, the factory floor might seem like a mystery. But the way a factory is laid out directly affects product quality, safety, and how fast your orders ship. In this article, we’ll walk you through the basics of supplement factory floor design and why it matters when you choose a supplement manufacturer. Let’s dive in.
Why Factory Floor Design Matters for Your Brand
A well-designed factory floor keeps production smooth and clean. It helps prevent cross-contamination and mix-ups. That means your private label supplements come out consistent every time.
Good design also speeds up production. When materials flow logically, there’s less waiting and fewer errors. This can lead to faster lead times and happier customers.
Finally, a smart layout makes it easier to meet strict standards. Many manufacturers aim for GMP-certified facility status. A clean, organized floor is a big step toward that.
Key Zones in a Supplement Factory
Most supplement factories are divided into specific zones. Each zone has a purpose and helps keep things organized.
Raw Material Storage
This is where ingredients are kept before use. It should be cool, dry, and pest-free. Ingredients are often labeled and tracked to avoid mix-ups.
Production Area
Here, ingredients are measured, mixed, and turned into final products. For example, a gummy manufacturer might have special cooking and depositing equipment. This area needs easy-to-clean surfaces and good airflow.
Packaging Zone
After production, products are bottled, labeled, and boxed. This zone should be separate to avoid contamination. It’s also where private label supplements get their final look.
Quality Control Lab
Every batch is tested here. The lab checks for potency, purity, and safety. This is crucial for halal supplement manufacturer compliance and overall trust.
Design Features That Make a Difference
Beyond zones, certain features improve how a factory runs. Look for these when you evaluate a supplement OEM partner.
- Unidirectional flow: Materials move in one direction, from raw to finished. This reduces the risk of contamination.
- Separate rooms: Different product types (like powders and gummies) have their own spaces. This avoids cross-contact.
- Easy-to-clean surfaces: Floors, walls, and equipment are made of smooth, non-porous materials. This makes cleaning faster and more effective.
- Proper ventilation: Good air handling keeps dust and moisture under control. It also helps maintain comfortable working conditions.
- Clear signage: Labels and signs guide workers and visitors. This reduces mistakes and improves safety.
These features might seem small, but they add up to big benefits. They help ensure your product is safe and meets regulations.
How to Evaluate a Manufacturer’s Floor Design
When you tour a factory or review a supplement manufacturer, ask about their layout. Here’s what to look for:
- Flow: Does the production flow logically from start to finish?
- Separation: Are different product lines kept apart?
- Cleanliness: Is the facility tidy and well-maintained?
- Certifications: Do they have GMP or halal certification? These show a commitment to quality.
- Capacity: Can they handle your order size without bottlenecks?
A good manufacturer will be proud to show off their floor. If they’re hesitant, that’s a red flag.
Why This Matters for Your Brand
Your reputation depends on product quality. A well-designed factory helps ensure every batch meets your standards. It also supports halal supplement manufacturer requirements if you’re targeting that market.
Plus, a smart layout can reduce costs. Less waste and faster production mean better pricing for you. That’s good for your bottom line.
Ready to find a manufacturer with a smart factory floor? Contact us for a free consultation and quote. We’ll help you turn your supplement idea into a reality.