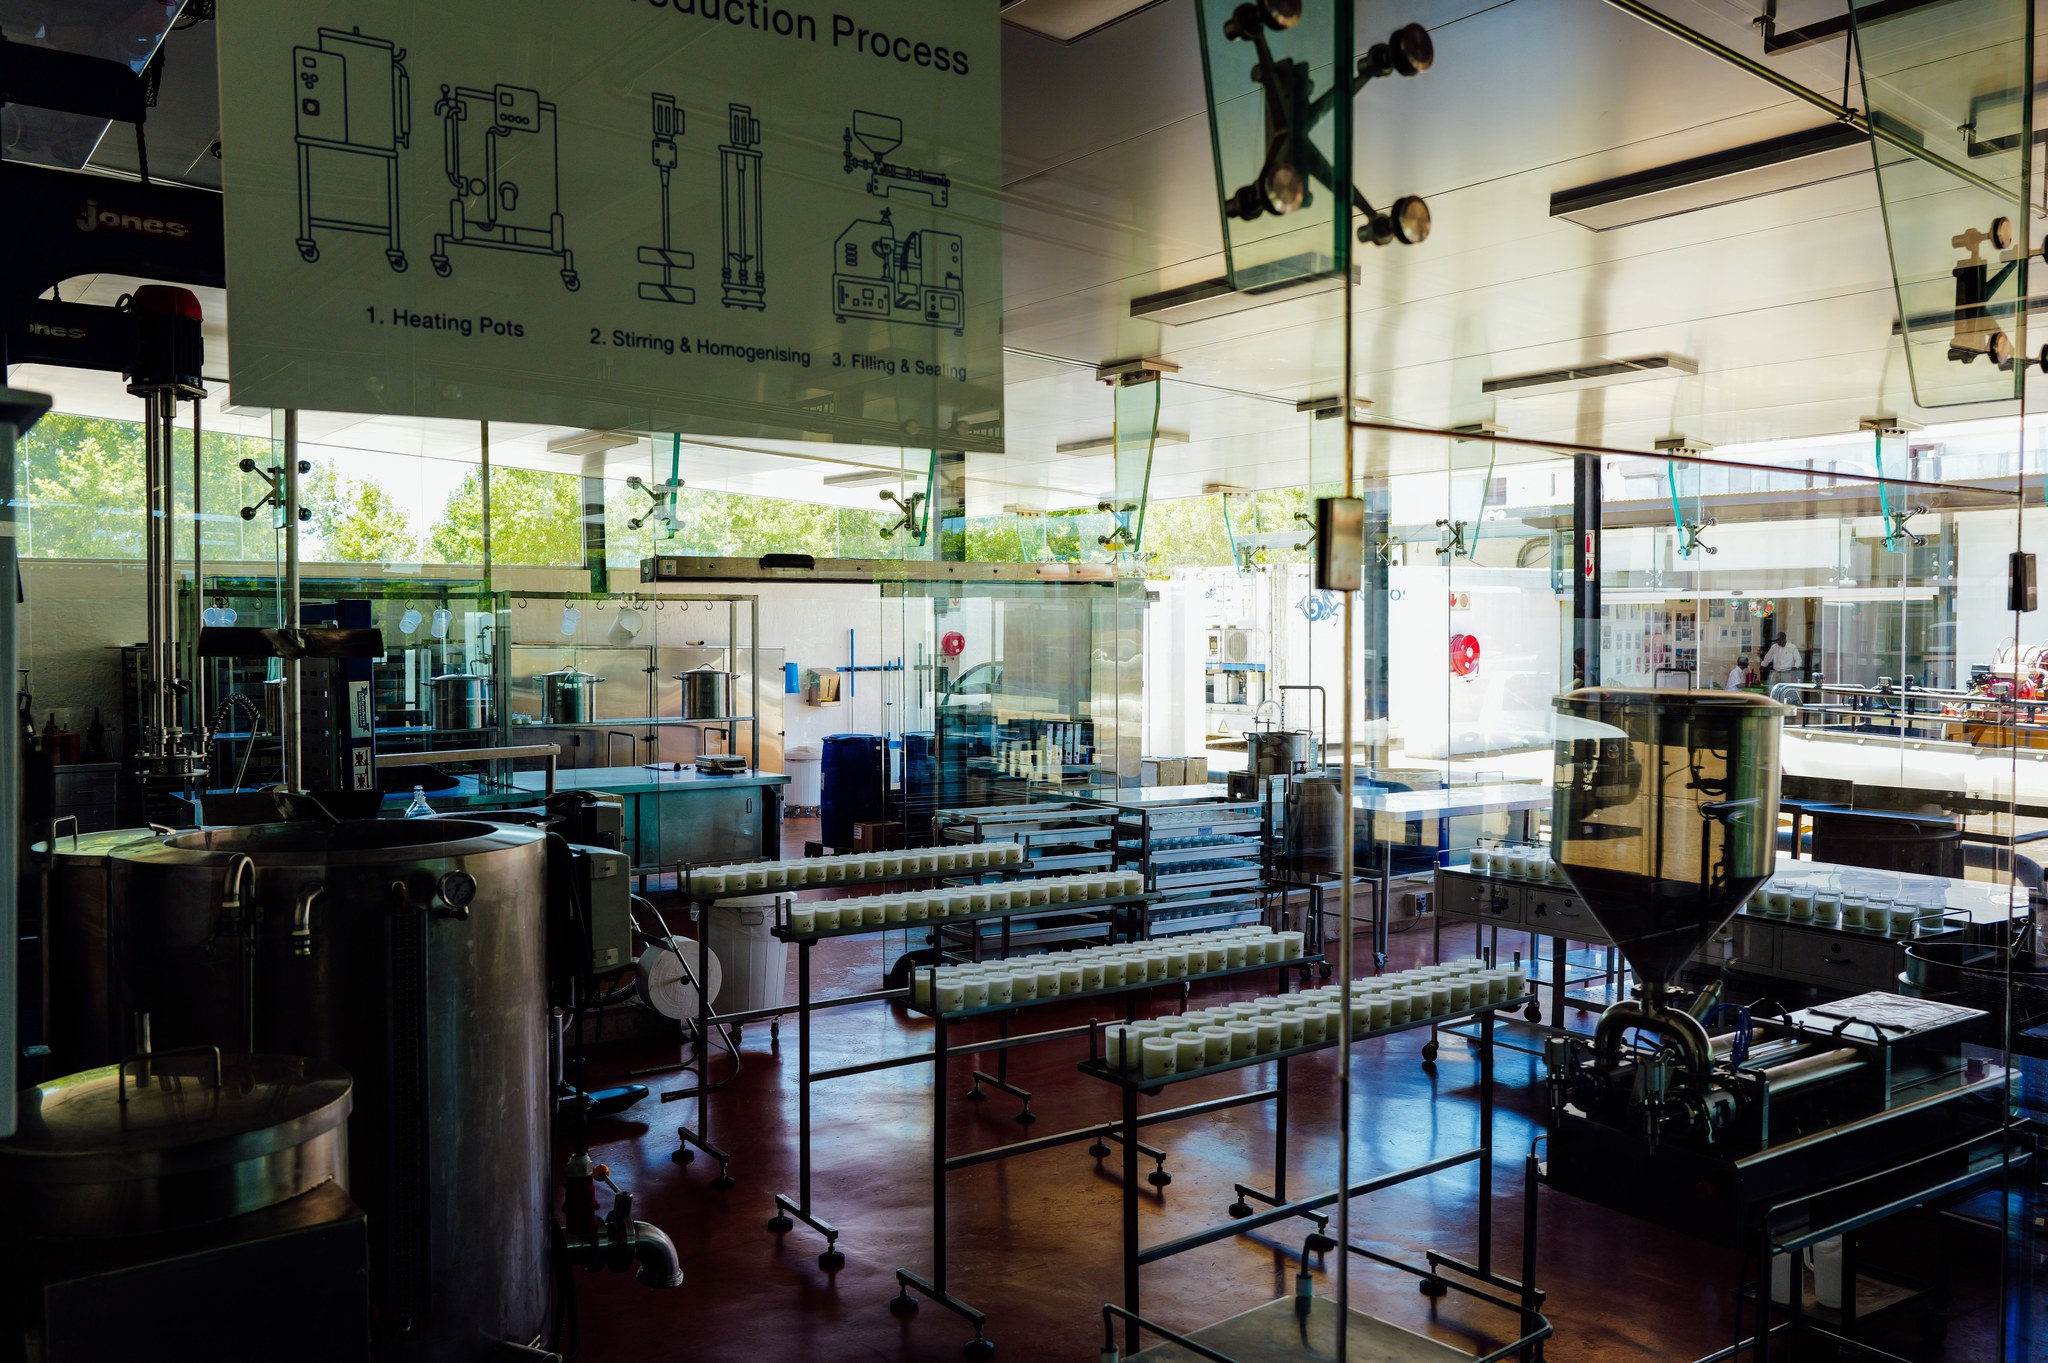
If you’re starting a supplement brand, you might not think about factory floor design. But it’s crucial. A well-designed floor ensures smooth production, high quality, and safety. In this guide, we’ll explain what goes into designing a supplement factory floor. You’ll learn why it matters and what to look for when choosing a supplement manufacturer.
Why Factory Floor Design Matters for Your Brand
The layout of a supplement factory directly affects product quality and safety. A good design prevents cross-contamination and ensures efficient workflow. It also helps meet regulatory standards. For you, this means reliable products that won’t harm your reputation.
When you choose a supplement OEM, ask about their floor design. A well-planned facility can handle different product types, from capsules to gummies. It also allows for private label supplements to be produced without mix-ups. This is especially important if you offer multiple products.
Moreover, a smart design reduces production costs. Efficient movement of materials and staff saves time and money. These savings can be passed on to you, making your brand more competitive.
Key Zones in a Supplement Factory
A typical supplement factory is divided into several zones. Each zone has a specific purpose and design requirements. Let’s look at the main ones.
Receiving and Storage
Raw materials arrive here. They’re checked and stored properly. Temperature and humidity are controlled to keep ingredients fresh. This zone must be separate from production to avoid contamination.
Production Area
This is where the magic happens. Ingredients are measured, mixed, and formed into final products. The layout depends on the product type. For example, a gummy manufacturer needs specific equipment for cooking and molding. The area must be clean and easy to sanitize.
Packaging and Labeling
Finished products are packaged here. The design ensures a smooth flow from production to packaging. This reduces the risk of errors and speeds up the process. Labeling must be accurate, especially for private label supplements.
Quality Control Lab
Samples are tested here. The lab checks for potency, purity, and safety. It should be close to production for quick testing. This helps catch issues early.
Warehouse and Shipping
Final products are stored and shipped from here. The area must be organized to prevent mix-ups. Proper storage conditions ensure product stability until it reaches customers.
Design Principles for a Top-Notch Facility
Good factory design follows several key principles. These ensure the facility runs smoothly and meets high standards.
- Unidirectional Flow: Materials move in one direction, from raw to finished. This prevents cross-contamination.
- Separate Zones: Different areas are physically separated. Walls or airlocks keep contaminants out.
- Easy to Clean: Surfaces are smooth and non-porous. This makes cleaning and sanitizing easier.
- Proper Ventilation: Good airflow removes dust and fumes. It also controls temperature and humidity.
- Safety First: Emergency exits, fire suppression, and safety equipment are essential.
These principles are critical for a halal supplement manufacturer. Halal requires no cross-contamination with non-halal substances. A well-designed floor helps maintain halal integrity.
What to Look for in a Manufacturing Partner
When choosing a supplement manufacturer, don’t just look at their products. Ask about their facility design. A good partner will be proud to show you their floor plan. They’ll explain how they prevent contamination and ensure quality.
Look for certifications like GMP (Good Manufacturing Practice). This shows they follow strict guidelines. If you need halal products, ensure they have halal certification. Also, ask about their low MOQ options if you’re just starting out.
Visit the factory if possible. See how the zones are laid out. Check if the flow makes sense. A well-designed factory is a sign of a reliable partner.
Remember, your brand’s reputation depends on the quality of your products. And that quality starts on the factory floor.
Ready to Start Your Supplement Brand?
If you’re looking for a reliable supplement OEM in Malaysia, we can help. Our factory is designed for quality and efficiency. We offer private label supplements and custom formulations. Whether you need capsules, tablets, or gummies, we’ve got you covered.
Contact us today for a free consultation and quote. Let’s bring your supplement idea to life!