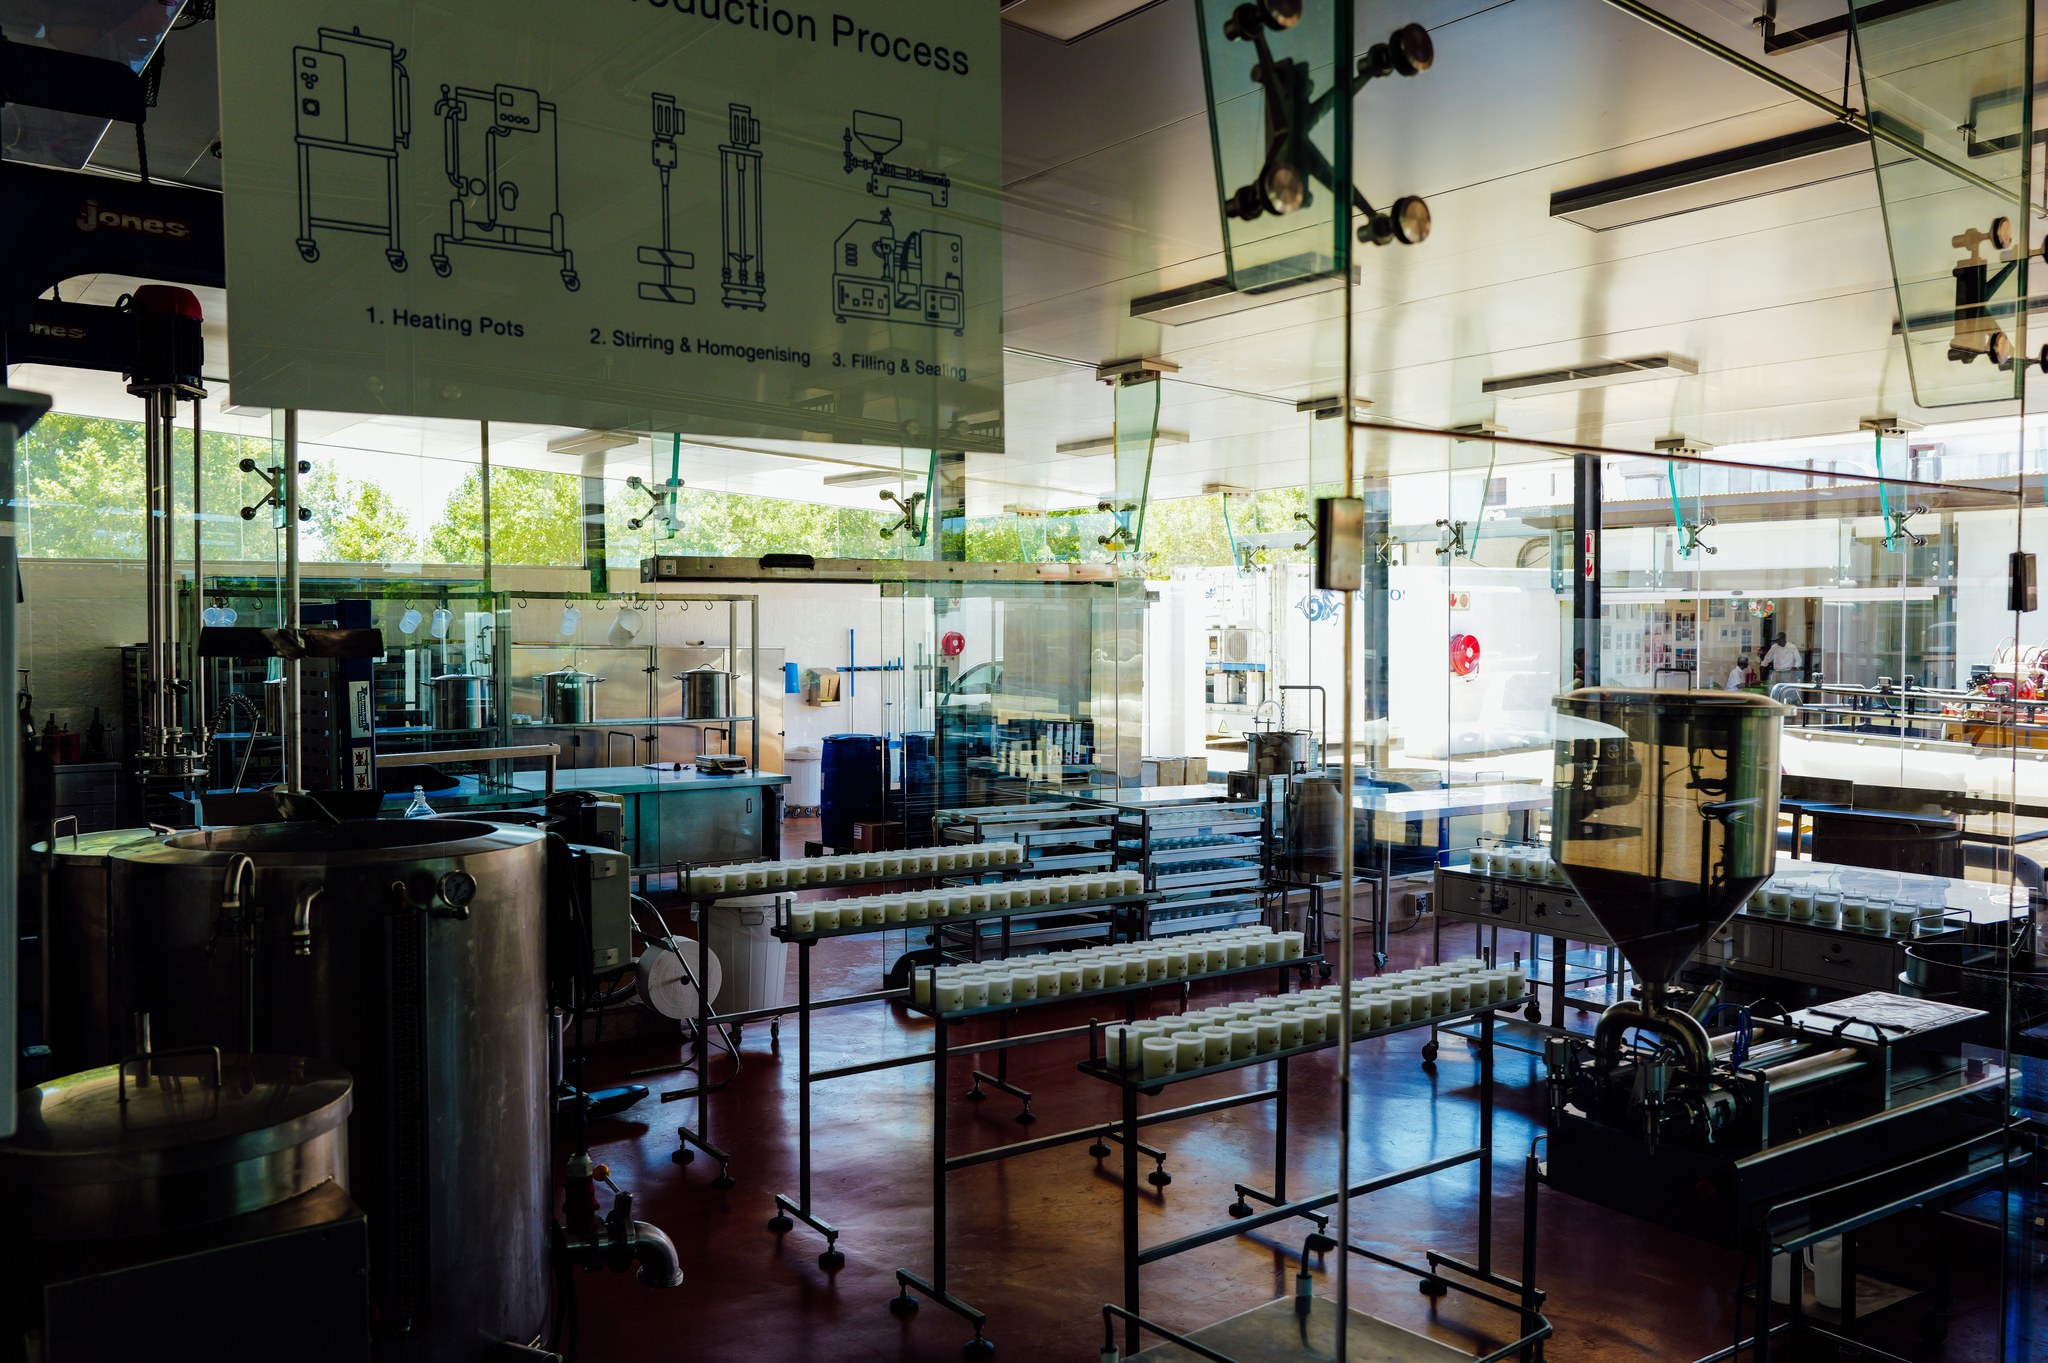
When you choose a supplement manufacturer for your brand, you might not think about the factory floor. But the design of the production area matters a lot. It affects product quality, safety, and even your costs. A smart floor plan keeps things clean and efficient. It also helps the factory meet important standards. In this article, we’ll explain what good supplement factory floor design looks like. You’ll learn why it matters for your private label supplements and how it can give you peace of mind.
Why Floor Design Matters for Your Supplement Brand
The floor layout is not just about where machines sit. It’s about the flow of materials and people. A well-designed floor reduces the risk of contamination. It also makes production faster and more reliable. For you, this means fewer delays and consistent product quality. A good layout also shows that the factory takes safety seriously. That’s a big plus when you’re choosing a partner for your brand.
Think about it: if the raw materials and finished products cross paths, there’s a risk. A smart design keeps them separate. This is a basic principle in good manufacturing practice, or GMP. A GMP-certified facility will have a floor plan that supports this separation. When you visit a factory, look at how they organize the space. It tells you a lot about their commitment to quality.
Key Elements of a Smart Factory Floor
A good floor design has several key parts. Each one helps keep your products safe and production smooth. Here are some things to look for:
- Zoning: The factory should have clear zones for different activities. For example, a separate area for weighing raw materials, another for mixing, and another for packaging. This prevents cross-contamination.
- Material flow: Raw materials should move in one direction, and finished goods should move out without crossing paths. This is often called a one-way flow.
- Air handling: Good ventilation and air filtration are crucial. They keep dust and particles from getting into your products. Look for positive air pressure in cleanrooms.
- Easy-to-clean surfaces: Floors, walls, and ceilings should be smooth and non-porous. This makes them easy to clean and disinfect. It also prevents bacteria from hiding.
- Adequate lighting: Bright, even lighting helps workers spot any issues. It also reduces the chance of mistakes.
These elements work together to create a safe and efficient production environment. When a factory has these in place, you can trust that your products are in good hands.
How Floor Design Supports Different Product Types
Different products need different setups. For example, making gummies is not the same as making capsules. A gummy manufacturer needs special equipment and a layout that handles sticky ingredients. The floor must be easy to clean to prevent buildup. Similarly, a factory that makes powders needs good dust control. The design should minimize dust in the air.
Gummy Production Areas
Gummy production involves heating and molding. The floor needs to be heat-resistant and non-slip. There should be separate areas for cooking, molding, and packaging. This helps manage temperature and humidity. A good gummy manufacturer will have a floor plan that supports these steps.
Powder and Capsule Lines
For powders and capsules, dust control is key. The floor should have smooth surfaces that don’t trap dust. There should also be a proper air filtration system. This keeps the environment clean and safe for workers. It also protects your product from contamination.
When you talk to a supplement OEM provider, ask about their floor design for different product types. This shows you that they understand the specific needs of each format.
Why You Should Choose a Factory with a Smart Floor Plan
Choosing a factory with a smart floor plan is a smart business move. It helps ensure your products are made safely and consistently. It also shows that the factory is serious about quality. This is especially important if you’re looking for a halal supplement manufacturer. Halal certification requires strict hygiene and segregation. A well-designed floor makes it easier to meet those requirements.
A good floor plan also supports efficiency. This can lead to faster production times and lower costs. That might mean a low MOQ for you, which is great for startups. You can start small and grow without worrying about quality issues.
Finally, a smart floor design makes it easier for the factory to pass audits. This gives you confidence that your products will meet regulatory standards. It also protects your brand’s reputation.
If you’re ready to start your own supplement line, we’re here to help. Our team can guide you through the process, from formulation to packaging. We have a modern facility with a smart floor plan. Contact us today for a free quote or consultation. Let’s create something great together!