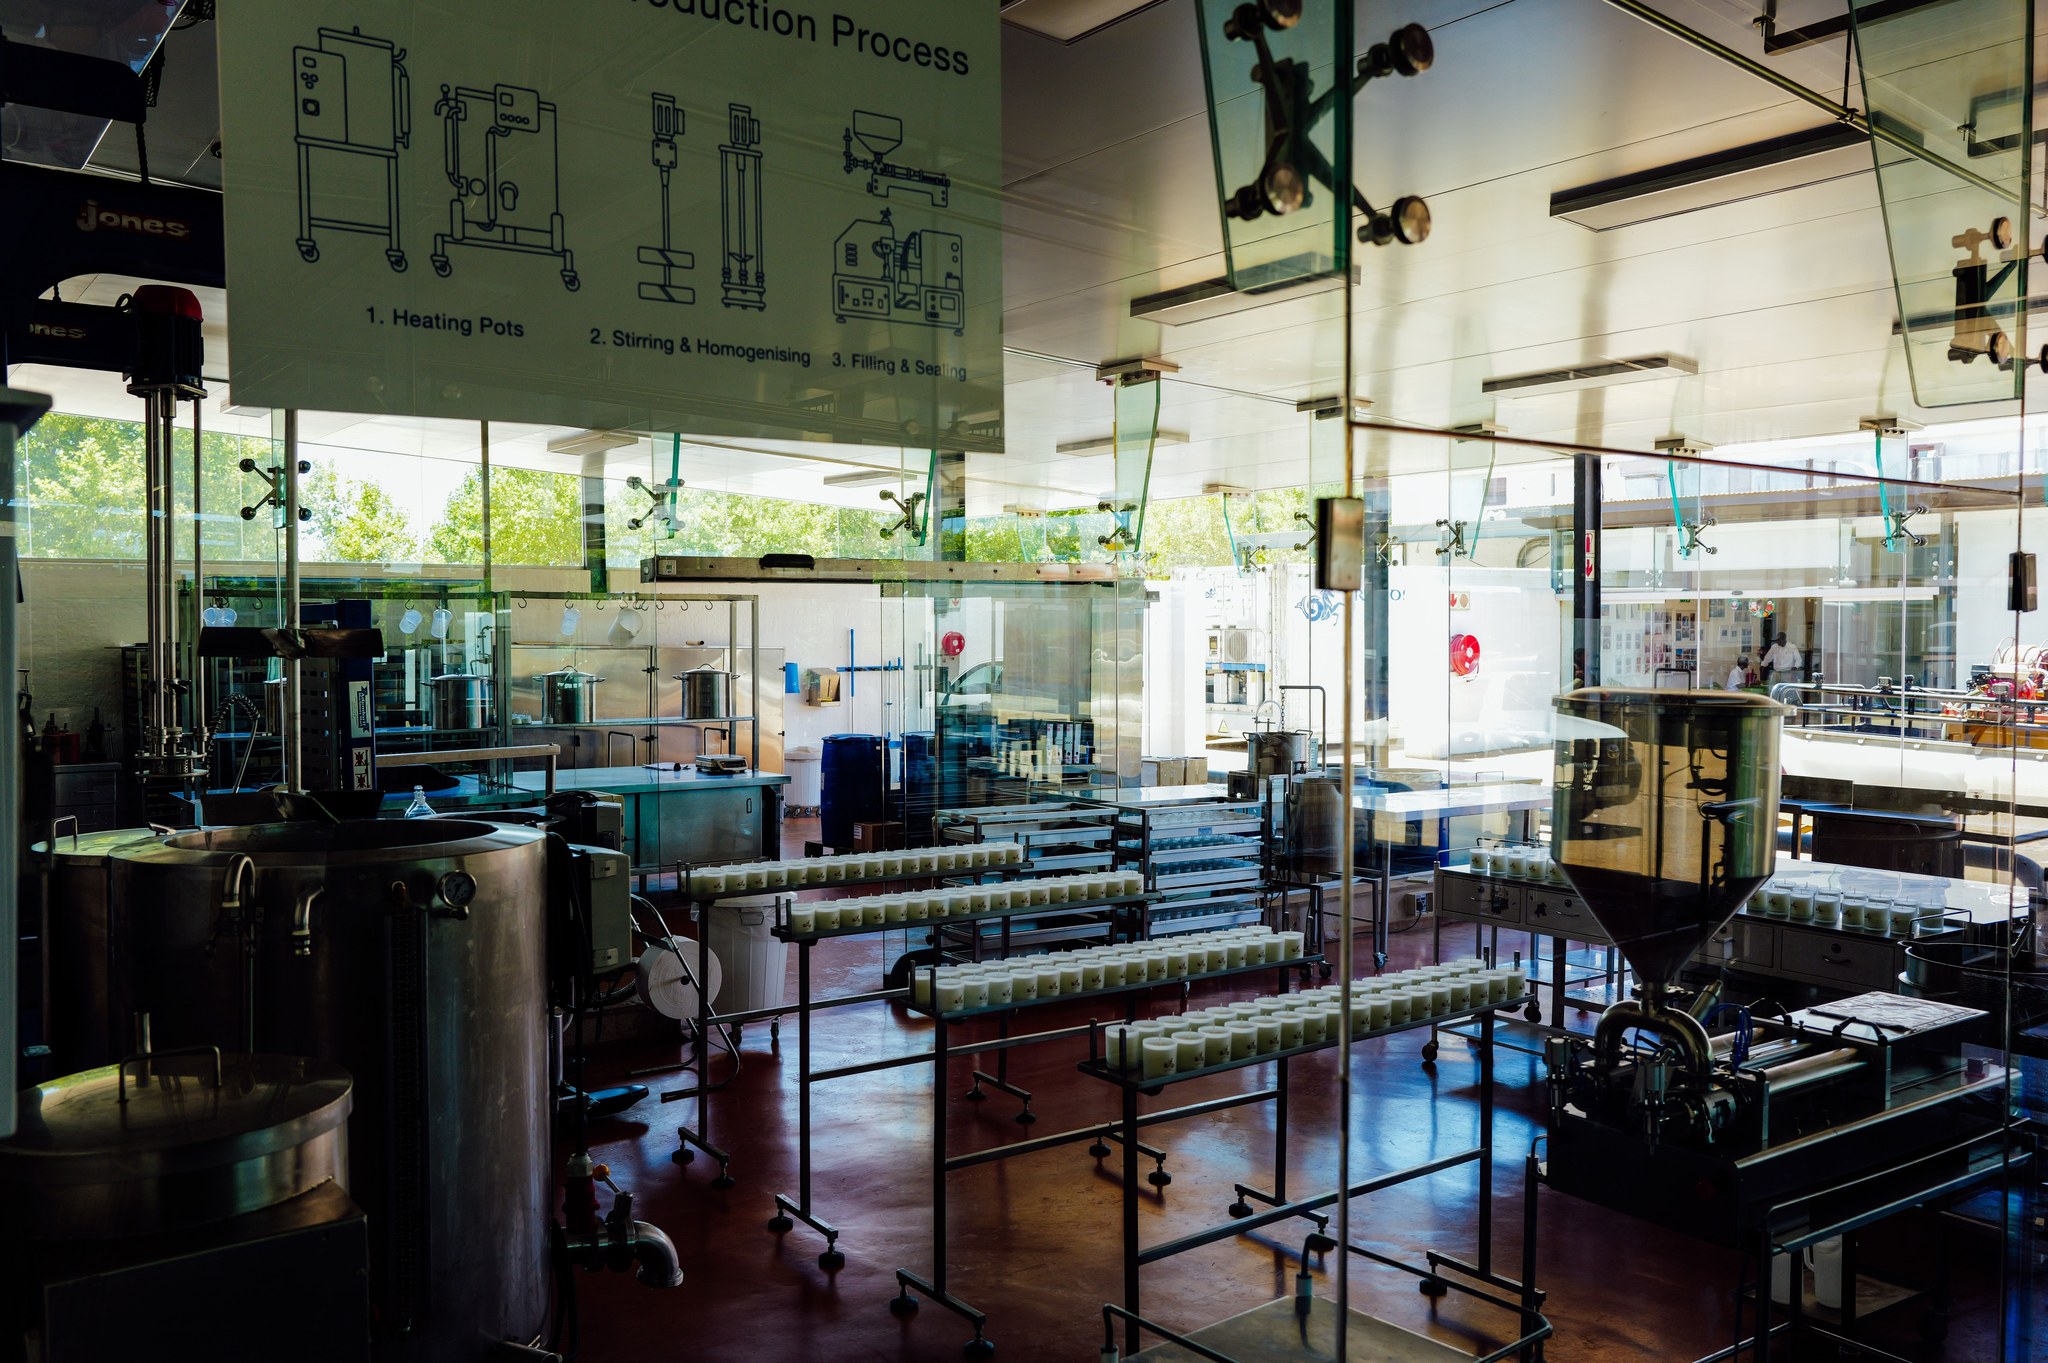
When you’re planning to launch your own supplement brand, the factory you choose matters a lot. But have you thought about the supplement factory floor design? It’s not just about looks. A smart layout keeps products safe, boosts efficiency, and helps you meet regulations. In Malaysia, more brands are turning to local OEM partners who understand modern factory design. Let’s break down what good floor design means for you and your product.
Why Floor Design Matters for Your Supplement Brand
Think of the factory floor as the heart of your production. If the flow is messy, mistakes happen. Cross-contamination, mix-ups, or delays can hurt your brand. A well-designed floor keeps raw materials, production lines, and finished goods separate. This protects your private label supplements from any quality issues. Plus, a clean, logical layout makes audits easier. You want a partner who treats floor design as seriously as you treat your brand.
Good floor design also supports halal supplement manufacturer requirements. Segregated areas and clear workflows help maintain halal integrity. This is key if you’re targeting Muslim consumers in Malaysia or globally. So, when you visit a potential OEM, look beyond the shiny machines. Check how the space is organized.
Key Zones in a Modern Supplement Factory
Every efficient factory has dedicated zones. Each zone has a purpose. Here are the main areas you’ll find in a well-designed facility:
- Raw material storage – Separate, climate-controlled areas for ingredients.
- Weighing and dispensing room – A clean space to measure and prepare materials.
- Production area – Where mixing, encapsulation, or tableting happens.
- Packaging line – For bottling, labeling, and final packing.
- Quality control lab – On-site testing to ensure every batch meets specs.
- Finished goods warehouse – Storing your products safely before shipping.
These zones must flow logically. For example, materials move from storage to weighing, then to production, then to packaging. This reduces backtracking and lowers contamination risk. A good supplement manufacturer in Malaysia will have this flow clearly mapped out.
Design Features That Support Quality and Safety
Cleanable Surfaces
Floors, walls, and ceilings should be smooth and easy to clean. No cracks or crevices where dust or bacteria can hide. This is a basic but vital part of supplement factory floor design. Look for epoxy-coated floors and sealed seams.
Proper Ventilation and Airflow
Air quality affects product stability and safety. Good HVAC systems control temperature and humidity. They also filter dust and particles. This is especially important for a gummy manufacturer, as gummies are sensitive to moisture and heat.
Segregated Utility Systems
Water, electricity, and compressed air should be designed to avoid contamination. For example, clean steam and water systems are separate from waste lines. This prevents any accidental cross-contact.
Adequate Lighting
Bright lighting helps workers spot issues. It also reduces errors during weighing and packaging. Plus, it makes inspections easier. Good lighting is a simple but often overlooked part of floor design.
How to Choose a Factory with Smart Floor Design
When you’re comparing supplement OEM partners, ask about their facility layout. Request a virtual or in-person tour. Look for clear separation between clean and dirty areas. Ask how they handle waste and air pressure. A trustworthy halal supplement manufacturer will be happy to explain their design logic.
Also, consider the type of product you want. If you’re into gummies, check if they have a dedicated gummy line with proper humidity control. If you’re doing capsules, see how they manage powder dust. The right floor design supports your specific product needs.
Remember, a factory with smart floor design isn’t just about compliance. It also helps with efficiency, which can lead to low MOQ options and better pricing for you. A smooth operation means less waste and faster turnaround. That’s a win for your brand.
Ready to find a factory that gets it right? We’re a Malaysian supplement manufacturer with a facility designed for quality and safety. Whether you’re exploring supplement OEM or private label supplements, we’d love to chat. Contact us today for a free quote or consultation. Let’s build your dream product together!